Co-extrusion: Rigid and Flexible in One Lighting Profile
Abstract: Co-extrusion puts two materials into one section in a single pass — a rigid body that holds the geometry and a flexible lip that seals it, or a clear light-exit face with an opaque light block behind it. It removes an assembly step and a part number, and it adds a second material stream, a more complicated die and a longer trial. This page sets out what co-extrusion genuinely buys, the three jobs where it is the right answer, where it is over-engineering, and the lines your drawing needs before it can be quoted.
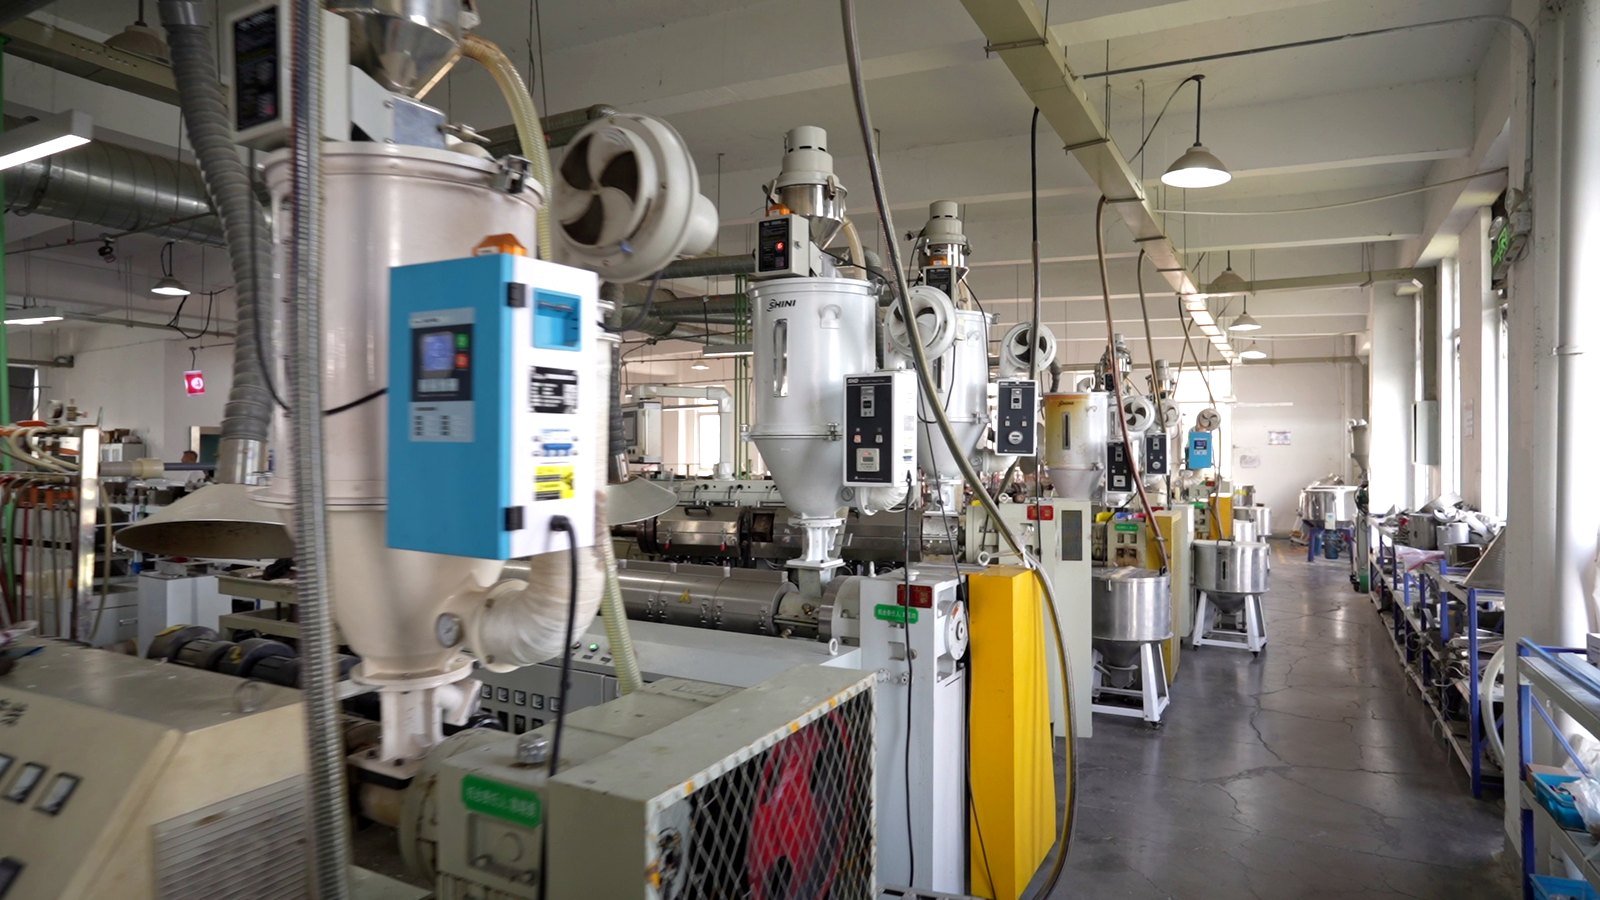
What it actually buys you
| Job | Single-material approach | Co-extruded approach |
|---|---|---|
| Sealing lip on a rigid housing | A separate gasket, bought, handled and fitted — often the part that goes missing on the line. | Flexible lip extruded onto the body. One part, one stock keeping unit, no assembly step. |
| Light block behind a lens | A second opaque profile or a painted insert, with its own tolerance stack. | Opaque and clear in one section, bonded in the die rather than afterwards. |
| Soft edge on a hard diffuser | Post-extrusion fitting, or a compromise on the single durometer. | Two durometers in one section, positioned exactly where the drawing needs them. |
The honest counterweight: co-extrusion is not free. It adds a second material to qualify, it makes the die more complicated and more expensive, and it lengthens the trial because two melt streams have to be balanced before the first article is worth measuring. Where a separate gasket is already in your bill of materials and already works, co-extrusion is usually over-engineering. Where the gasket is the part that causes assembly problems, it pays for itself.
Four ways a co-extruded section goes wrong
What to put on the drawing
- Which zone is which material, marked on the section view, not described in a note.
- Material specification for each zone — grade intent, colour, and any flame or compliance requirement per material.
- The function of the flexible zone: sealing, grip or edge protection — stated as compression, not as a nominal dimension.
- Bond-line location and whether the joint must be invisible on the visible face.
- Compliance documentation per material, because a yellow card for one stream does not cover the other.
- Wall thickness at the thinnest point in each zone.
Why the trial takes longer than a single-material section
Buyers who have run both usually notice one difference immediately: the first article on a co-extruded section takes more passes. That is not a supplier problem, it is what balancing two melt streams involves.
- The two materials want different conditions. Melt temperature, viscosity and cooling rate differ, so the die has to be tuned to a compromise that keeps both where the drawing wants them.
- The bond line has to be positioned, not just produced. Where the two materials meet is a dimension. Moving it means changing land geometry, not changing a setting.
- Shrinkage differs between the zones. A rigid body and a flexible lip do not shrink the same way, so the section can come off the line straight and settle out of shape — or the reverse.
- Two material lots to qualify. Each stream needs its own data sheet, colour check and any compliance documentation the market requires, and that is per order, not per die.
The practical implication: plan the sample stage honestly. A co-extruded section that is quoted on a single-material timeline is usually a co-extruded section that will be re-quoted.
Four questions buyers ask before committing
Lead time and cost, stated plainly
A co-extruded section follows the same path as any custom profile — drawing review, die design and manufacture, first-article samples with measurement, then production after approval, roughly six weeks from an approved drawing to first production parts — with the trial stage lengthened by the second stream. Minimum order quantity is 500 units. Two materials also means two lots to trace, which is worth stating in the batch documentation clause.
Frequently asked
Is a co-extruded profile stronger than a single-material one? Not inherently. Co-extrusion changes what the section can do at a given place — seal here, transmit light there — it does not make the body stronger. Structural questions are still answered by wall thickness, geometry and support spacing, and those belong on the drawing either way.
Can the flexible zone be a different colour from the body? Yes, and it often is, for a visible gasket line or a light block. Specify colour per zone, and expect a separate colour clause and a separate ΔE reference for each. One colour clause covering two materials is a clause that will be argued about later.
Does co-extrusion change the compliance position? It adds one. Each material needs its own documentation — a flame rating on the rigid stream does not cover the flexible one, and a RoHS report that names one polymer does not describe the other. State the documents you need per zone.
What if the section later needs to be simplified? Going the other way is easier: a co-extruded section can often be re-cut as a single material with a separate gasket, because the body geometry already exists. The reverse — adding a second material to an existing die — is a new die. If there is any chance the brief will change, say so before the tooling is cut.
Related reading: custom lighting extrusion capability, tooling, what you actually pay for in tooling, and die lifecycle and ownership. Have a section to compare? send the drawing.